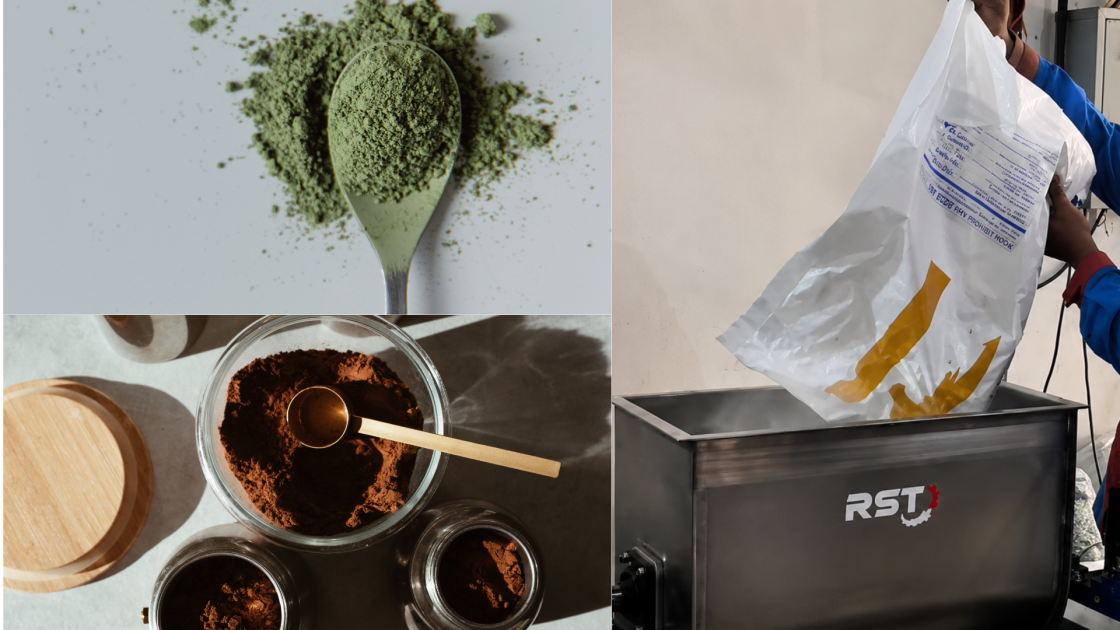
Looking to Scale Up Your Powder Drink Business? A Ribbon Mixer and Screw Conveyor Could Be the Solution
Discover how ribbon mixers and screw conveyors help powder drink manufacturers scale production, improve mixing consistency, and optimize material handling.
Many powder drink businesses—including instant drink powders, powdered herbal drinks, instant coffee and tea, and powdered health beverages—start production manually. Ingredients are mixed by hand, using household mixers, or with simple equipment suitable for small-scale operations.
This approach can work well when production volumes are limited. However, as the business grows, orders increase, distributor demand rises, and products enter modern retail channels, traditional production methods may no longer be sufficient.
The challenge is not just about mixing ingredients. It is also about how materials move efficiently between production stages.
This is where a combination of a ribbon mixer and screw conveyor can support the transition from small-scale production to industrial manufacturing.
Why Manual Production Becomes a Bottleneck as Your Business Grows
Common challenges faced by powder drink manufacturers using manual mixing and material handling include:
- Production time cannot keep up with demand: Repeated mixing using small equipment takes longer when production volumes increase.
- Inconsistent mixing results: Manual mixing depends heavily on operator technique, making batch-to-batch consistency more difficult to maintain.
- Manual material handling: Mixed powder often needs to be transported using buckets, trolleys, or manual lifting, increasing handling time and the risk of spillage.
- Challenges in production standardization: Businesses preparing for food safety requirements and relevant certifications may benefit from more controlled and documented production processes.
- Increasing labor costs: As production volume grows, manual mixing and material transfer can become less efficient compared with appropriately designed industrial equipment.
What Is a Ribbon Mixer?
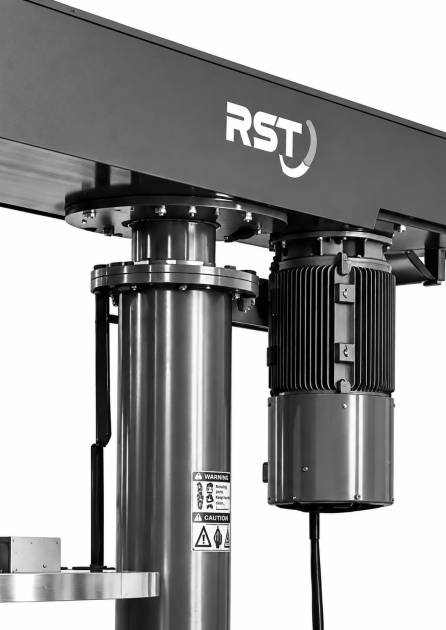
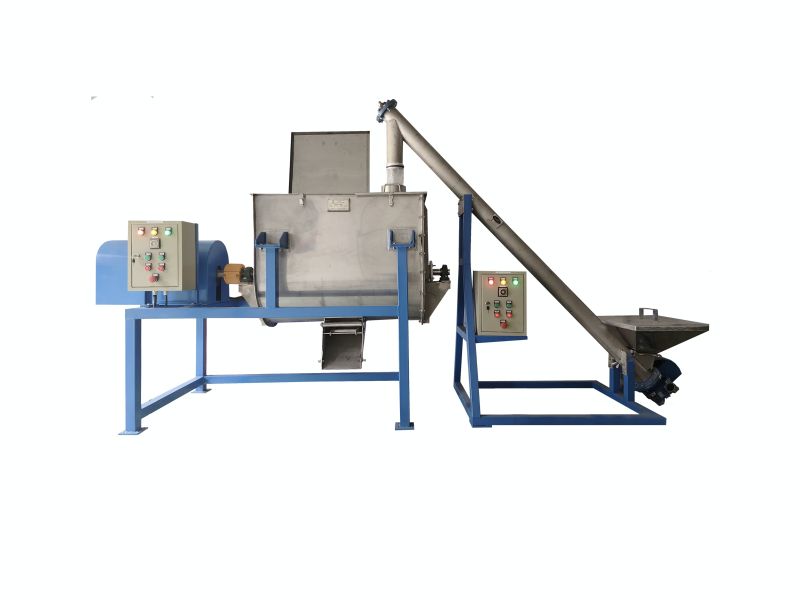
A ribbon mixer is a horizontal industrial mixing machine that uses double ribbon-shaped agitators rotating inside a U-shaped mixing chamber.The ribbon design creates a movement pattern that helps blend powder ingredients throughout the mixing chamber. In powder drink production, the ingredients may include sugar, powdered flavors, coloring agents, vitamins, and other formulation components.
A properly selected and designed ribbon mixer can help manufacturers achieve consistent mixing performance at larger production volumes. However, mixing is only one part of the production process. After the powder has been mixed, the next challenge is transferring the finished product to a packaging machine, storage hopper, silo, or another production stage.
This is where a screw conveyor becomes an important part of the production system.
What Is a Screw Conveyor?
A screw conveyor is a material handling system that uses a rotating screw or auger inside a trough or enclosed tube to transport powder and granular materials. Depending on the production layout, a screw conveyor can be designed for horizontal, inclined, or other suitable transfer configurations.
In powder drink manufacturing, a screw conveyor may be installed after the ribbon mixer to transfer blended powder to a discharge point, packaging machine, hopper, or temporary storage system. An enclosed screw conveyor design can help reduce direct exposure to the surrounding environment, minimize material spillage, and support cleaner material handling. Its suitability depends on the product characteristics, equipment design, and required hygiene controls.
Why Combine a Ribbon Mixer and Screw Conveyor in One Production System?
Integrating a ribbon mixer with a screw conveyor can provide several operational advantages:
1. Integrated Production Flow
The blended material can be transferred from the ribbon mixer to the next production stage through a connected material handling system, reducing unnecessary manual handling.
2. Reduced Manual Material Handling
A screw conveyor can reduce the need to move powder using buckets or trolleys, helping improve workflow efficiency as production volumes increase.
3. Better Control of Product Handling
The transfer system should be designed according to powder characteristics and the required handling conditions to help minimize segregation and preserve the quality of the blended material.
4. Improved Hygiene and Dust Control
Enclosed material transfer can help reduce spillage and exposure to the surrounding production environment. Additional dust collection and hygiene measures may be required depending on the product and facility requirements.
5. Flexible Production Layout
Screw conveyors can be configured according to the distance, elevation, and layout between the mixing machine and the next production stage.
6. Matching Mixing and Transfer Capacity
The ribbon mixer and screw conveyor should be selected and sized together to support the required production rate and minimize bottlenecks between mixing and material transfer.
7. More Efficient Production Cycles
An integrated mixing and material handling system can help reduce unnecessary handling steps and improve overall production workflow.
Signs Your Powder Drink Business Is Ready for an Upgrade
Your business may need to evaluate industrial mixing and material handling equipment when:
- Regular orders exceed your current manual production capacity.
- You begin receiving larger orders from distributors or retail customers.
- Batch-to-batch consistency becomes difficult to maintain.
- Transferring blended powder to the packaging machine takes too much time.
- Powder dust and material spillage are frequent issues in the production area.
- You are preparing for relevant food safety certifications and more standardized production procedures.
- Manual labor costs are becoming a significant part of production expenses
How to Choose the Right Ribbon Mixer and Screw Conveyor
Not every powder drink manufacturer needs the same equipment specifications. Several factors should be considered before selecting your ribbon mixer and screw conveyor.
Production Capacity
Evaluate your current daily and weekly production volume, as well as your expected business growth over the next one to two years.
The equipment should be selected based on actual batch size, production targets, material characteristics, and operating requirements.
Product Formulation and Number of Variants
If your business produces multiple flavors or formulations, equipment cleanability and access for maintenance are important considerations to help reduce the risk of cross-contamination.
Factory Layout
The screw conveyor configuration should match the positions of the ribbon mixer, packaging machine, storage hopper, and other production equipment
Transfer Distance and Elevation
The required conveyor length, inclination, and transfer capacity depend on the distance and height between the mixing and receiving points.
Future Certification Requirements
If you plan to pursue BPOM registration, halal certification, or other applicable standards, consider equipment design, documentation, cleanability, and process controls early in the planning stage.
Ribbon Mixer and Screw Conveyor Solutions from PT Rho Sigma Trijaya
PT Rho Sigma Trijaya (RST) is an industrial mixing and tank equipment manufacturer based in Tangerang, Indonesia.
We help powder drink manufacturers—from growing small and medium-sized businesses to industrial-scale operations—evaluate and develop integrated ribbon mixer and screw conveyor systems based on their production requirements, future growth plans, and material handling needs.
Our equipment solutions can be customized based on:
- Mixing capacity and production requirements
- Product-contact materials, including stainless steel options
- Screw conveyor configuration and transfer distance
- Discharge and material handling requirements
- Production layout and equipment integration
RST provides custom engineering and fabrication solutions for industrial mixing and process equipment applications.
Conclusion
Scaling powder drink production involves more than increasing labor or expanding your production area.
It requires a production system that can handle higher volumes while supporting consistent mixing performance and efficient material handling.
A ribbon mixer addresses the need for industrial powder mixing, while a screw conveyor supports efficient transfer between production stages.
When designed as an integrated system, these two types of equipment can help powder drink manufacturers improve their production workflow and prepare for future business growth.
Ready to Scale Your Powder Drink Production?
Looking for a custom ribbon mixer and screw conveyor system for your powder drink manufacturing business?
Talk to the engineering team at PT Rho Sigma Trijaya.
???? Website: https://www.rhosigmatrijaya.co.id/
Let's discuss your production requirements.
Frequently Asked Questions (FAQ)
1. What equipment is needed to scale up powder drink production?
Common equipment may include an industrial ribbon mixer, screw conveyor, screening equipment, packaging machinery, and other supporting systems. The exact equipment depends on the product formulation, production capacity, hygiene requirements, and factory layout.
2. What is a ribbon mixer and how does it work?
A ribbon mixer is a horizontal industrial mixing machine with ribbon-shaped agitators that rotate inside a mixing chamber. It is commonly used for blending powder and granular materials, subject to suitable equipment selection and product characteristics.
3. What is a screw conveyor used for in powder drink production?
A screw conveyor transports powder or granular materials from one production stage to another. It can be designed for horizontal or inclined transfer, depending on the required layout and material characteristics.
4. What should be considered when selecting a screw conveyor?
Key considerations include material properties, required transfer capacity, distance, elevation, conveyor configuration, production layout, cleanability, and future production requirements.